Year Established: 1970
ISO 9001:2015 Quality System
ISO 9001:2015 Quality System
Home > Mechanical Plating
Protect critical components with specification-driven mechanical plating in NJ. Mechanical Galvanizing provides non-electrolytic barrel finishing for manufacturers and distributors nationwide.
We process customer-supplied hardware across regional manufacturing hubs, from high-volume assembly lines to machine shops needing protective finishes on threaded studs in NJ. Our room-temperature barrel process deposits uniform metallic coatings that preserve pitch diameters, prevent heat distortion, and deliver dependable corrosion protection.
Established in 1970 | ISO 9001:2015 Quality System | Trenton, New Jersey Facility
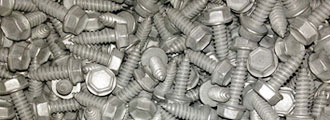
Mechanical plating is a cold-finishing process that bonds protective metals to steel and iron parts using kinetic energy without electrical current. Customer-supplied components tumble in an open barrel with glass impact media, water, metal powder, and promoter chemistry. The media mechanically cold-welds metal particles onto the substrate. Because current is absent, deposition remains uniform across edges, recesses, and root diameters, ensuring predictable fit on high-strength fasteners and stamped hardware without excess edge buildup.
Explore ten practical advantages of mechanical finishes for hardened fasteners, flat stampings, springs, and demanding industrial hardware.
We apply functional metallic coatings matched to your engineering drawings:
Provide your required metal, thickness class, and applicable ASTM or OEM specification for an accurate quote.
Whether managing high-volume finishing for fasteners or receiving freight from national accounts, our Trenton lines handle barrel-compatible components:
Part suitability depends on piece weight, longest dimension, geometry, and target coating thickness.
1. Clean and Prepare: Chemical cleaning removes oils, scale, and surface oxides so the base metal accepts the coating.
2. Load the Barrel: Clean parts enter the barrel with glass media, water, promoter chemistry, and the specified metal powder.
3. Mechanically Deposit: Controlled rotation drives the media to cold-weld metal particles onto the substrate to the target thickness.
4. Finish and Inspect: Parts receive specified conversion coatings, sealers, torque lubricants, or dyes, followed by lot thickness verification.
We process coatings to ASTM B695 and B696 standards, drawing notes, and OEM specifications. By evaluating base hardness, thread pitch, and mating tolerances upfront, our team applies compatible conversion chemistries and torque-control sealers so finished parts install reliably in automotive, construction, and industrial assemblies.
Submit your component prints to our engineering team for technical review and pricing:
What is the technical difference between mechanical plating and mechanical galvanizing?
Both use identical mechanical barrel principles. Mechanical plating designates thinner deposits (0.0002 to 0.0007 inches / 5 to 18 microns) for precision fasteners and clips. Mechanical galvanizing covers heavier deposits, typically ASTM B695 Class 25 (0.001 inches) and higher, for exterior utility and structural hardware.
How do out-of-state manufacturers ship parts to your Trenton facility?
Customers ship parts in drums, crates, or boxes via LTL carriers or parcel services directly to our receiving docks. We verify counts, run production, and coordinate return freight or carrier pickup.
Can you supply Certificates of Conformance with finished lots?
Yes. We provide Certificates of Conformance confirming that the applied coating satisfies your specified ASTM standard, drawing note, thickness class, or purchase order requirements.
Are there minimum order charges or lot size limits?
We process small trial batches and multi-ton production runs. Because each barrel run requires dedicated chemistry, media staging, and line setup, standard minimum lot charges apply.
What factors affect project pricing and lead times?
Pricing and lead times depend on incoming surface condition, cleaning cycles, metal selection, coating thickness class, and post-plate sealers or lubricants. Complete drawings submitted upfront ensure rapid quoting.
Can we run first-article samples before full production?
Yes. We process sample lots so your quality team can verify coating distribution, thread fit, torque performance, and visual finish before releasing full production quantities.